At West River, we understand that efficiency, price, and equipment durability are your leading concerns when purchasing conveyor equipment. We are committed to building quality products by listening to and understanding our customers’ needs.
Conveyor Systems
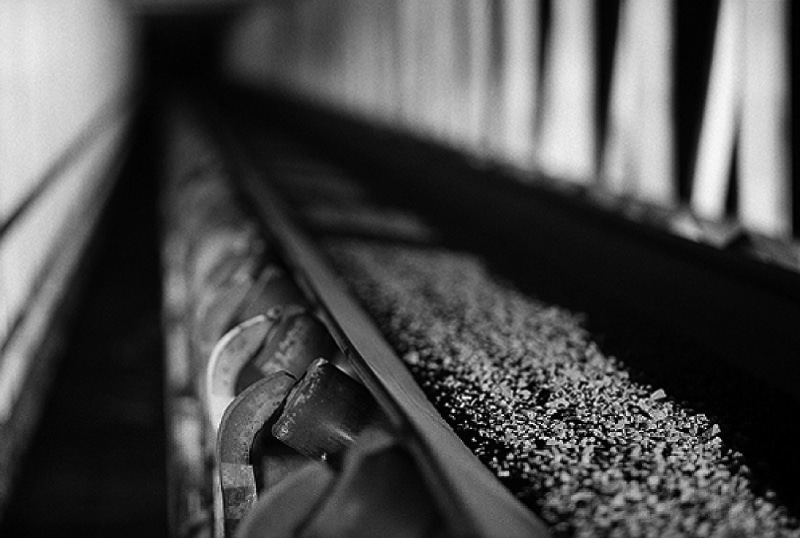
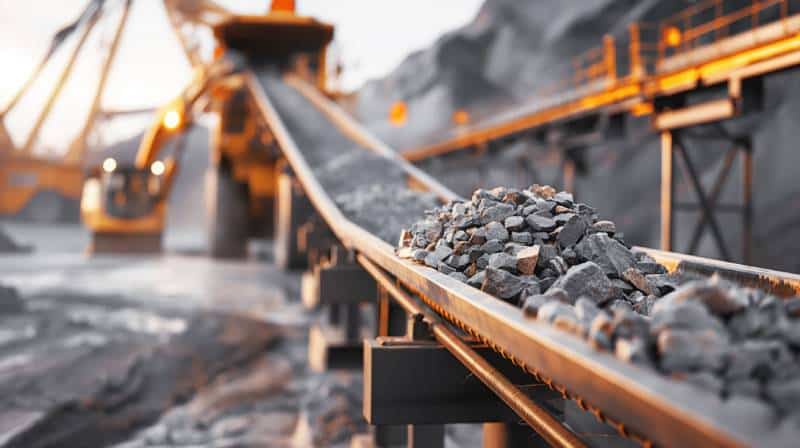
West River builds durable, custom conveyor systems for the mining industry. Our conveyors are engineered to efficiently and safely transport copper, coal, salt, potash, and precious metal ores.
Our rugged conveyors withstand the mining industry’s challenges.
Long runs
High temperatures
Uphill hauls
Heavy, abrasive materials
Dirty or dusty environments
We build our custom conveyor systems tough and can provide a complete turnkey conveyor package or individual conveyor system components and parts.
Underground mining conveyor systems must be high-quality due to the combination of dust, dirt, and confined spaces. These systems are also subject to various complex OSHA, MSHA, and state regulations.
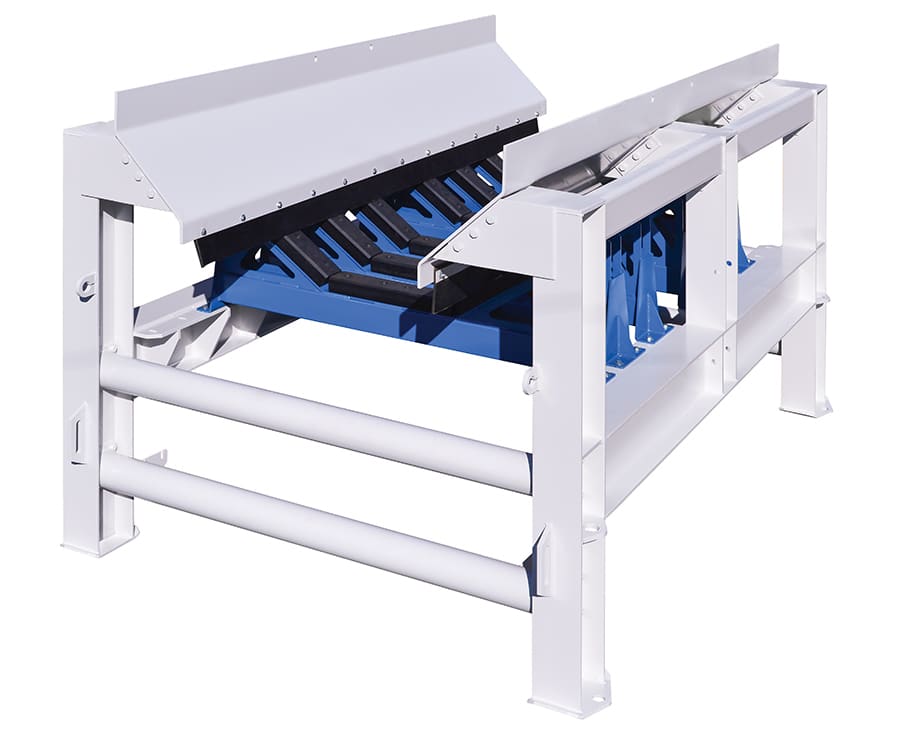
We offer a variety of conveyor structures and belt options to meet your underground mining needs, such as conveyor structures, belts, terminal equipment, and accessories.
Every underground application is different—ask us about custom equipment packages tailored to your needs.
Move massive quantities of bulk materials from their source to stockpiles or processing facilities with overland conveyors, and keep operational costs and disruptions to a minimum.
Our customizable used and rebuilt conveyors are a prime option for managing your mining equipment needs. They offer many benefits our customers have come to appreciate, such as cost savings and customization.
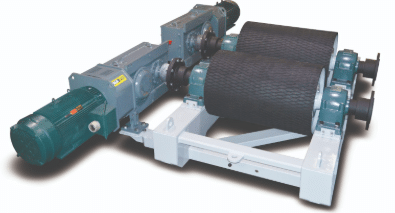
In addition to manufacturing our products, such as custom conveyor belt drives, we carry a wide assortment of terminal equipment from industry-leading brands. We can provide you with new, used, and rebuilt components and build whatever you need to your specifications.
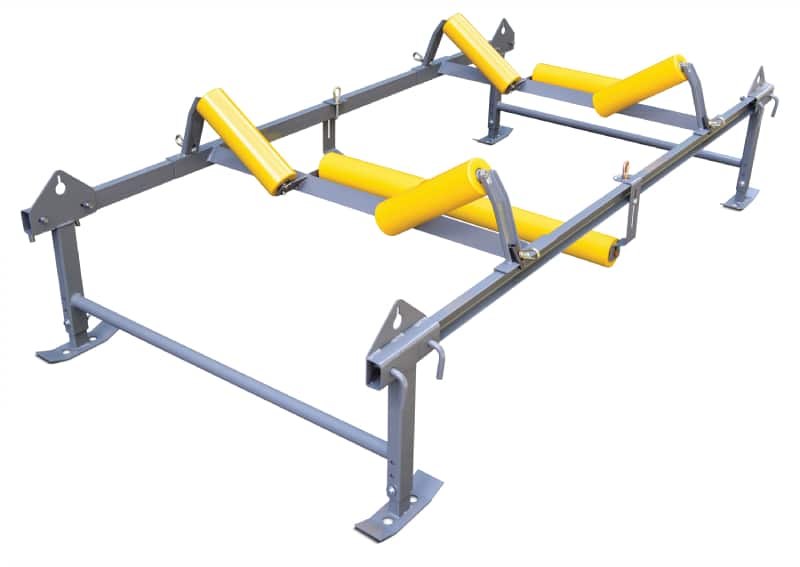
West River’s structure comes in CEMA B, C, D, E, and E+ and can be used for longwall and room-and-pillar operations. If conveyor specifications are provided, we can provide engineered idlers upon request.
Abrasive materials, heavy loads, and environmental factors can all contribute to conveyor belt failure. West River Conveyors offers underground and surface mining conveyor belts that can withstand the rigors and prevent unplanned downtime.
“I would like to express my appreciation and gratitude for the exceptional support provided by Russ during a recent troubleshooting effort. His availability, technical expertise, and proactive approach were instrumental in resolving the issues efficiently and effectively. Russ’s dedication to fostering and maintaining strong, long lasting professional relationships surpasses the typical sales mentality I have grown used to dealing with elsewhere. His commitment to his customers and consistent follow through has built a foundation of trust that I professionally continue to rely on. Having someone so dependable and relationship focused adds tremendous value, and it speaks volumes about the culture and professionalism of West River as a whole. Please extend my appreciation to Russ for his outstanding work and continued partnership.”
– Regina Tuberville, Sr. Mine Engineer
“I have had excellent success with everything I have purchased from West River. The service is great! I have called after hours and received the same top-notch service. The pulleys that I bought have been top-quality and are doing very well. I recently had some alignment work done on our slope belt, with the same high quality workmanship. I would recommend West River to anyone needing gearboxes, pulleys, alignment, or other conveyor components.”
– Steve Bjork, Preparation Plant Maintenance Chief
“West River is a friend to the mining industry, supplying quality components at a competitive price!”
– Barry Tackett, Operations Manager, Mountain Aggregates
“From the beginning, we wanted to standardize our conveyor equipment. We knew we wanted to minimize the number of spare parts and pulleys. This has been the only time in my career I’ve been able to accomplish this task. The good relationship that we’ve developed with West River is attributed to the genuinely good people that run the company. In my experience, many vendors are primarily interested in maximizing their profit margin but I truly believe the team at West River has the best interest of the customer at heart.”
– Brad Rigsby, General Manager, Black Panther Mining
“West River’s conveyor systems have given us a great level of reliability. In the years that we have been using them as our supplier, we have not had a single breakdown, no quality issues, and no under-design problems. West River’s dedication to excellence in customer service is exceptional. All phone calls and emails are replied to in a timely manner and deadlines are always met even when they may seem unachievable.”
– Coley Burgess, Mine Engineer, Mosaic Company
Our Process
Our certified engineers use cutting-edge technology to design and manufacture all our conveyor products on-site. We exercise strict quality control measures to ensure complete customer satisfaction with every product that leaves our facility.
We streamline our job processes to increase productivity and build your conveyor components promptly. Our investment in a PCR42 Structural Steel Plasma Cutting Robot enables more precise cutting and drilling.
“Quality is never an accident; it is always the result of high intention, sincere effort, intelligent direction, and skillful execution.”
Conveyor Parts for the Mining and Aggregate Industries
At West River, we have over 40 years of experience building custom conveyor systems for the mining and aggregate industries. We realize that each application is unique, and we can provide you with specialized or custom parts from major manufacturers to keep your conveyor equipment running.
West River Conveyors will design, build, and install your application’s customized dirt conveyor system. With over 40 years of experience, our expert engineers will help solve your toughest material-moving challenges. Our superior conveyor belt solutions enhance the safety and efficiency of your mining operations. Contact West River Conveyors today to discuss your requirements and discover how our products can contribute to your operational success.
For most mining operations, the relationship with a conveyor supplier ends at commissioning. The system is installed, it runs, and the paperwork gets filed away. At West River Conveyors, that's read more »
Leaching is often discussed in terms of chemistry—solutions, reactions, and recovery rates. But behind every successful operation is a material handling system that keeps everything moving at the right pace. read more »
When a conveyor system isn’t performing as expected, the first instinct is often to look at belt speed, capacity, or wear components. But in many cases, the issue starts upstream—inside read more »
This website uses cookies to improve your experience. We'll assume you're ok with this, but you can opt-out if you wish. Cookie settingsACCEPT
Privacy & Cookies Policy
Privacy Overview
This website uses cookies to improve your experience while you navigate through the website. Out of these cookies, the cookies that are categorized as necessary are stored on your browser as they are as essential for the working of basic functionalities of the website. We also use third-party cookies that help us analyze and understand how you use this website. These cookies will be stored in your browser only with your consent. You also have the option to opt-out of these cookies. But opting out of some of these cookies may have an effect on your browsing experience.
Necessary cookies are absolutely essential for the website to function properly. This category only includes cookies that ensures basic functionalities and security features of the website. These cookies do not store any personal information.