Are your conveyor belts taking a beating from the materials you’re moving? Some materials and product are more demanding than others. Materials that are heavy, sharp or unusually shaped have the potential to really wreak havoc on conveyor belts and conveyor structure.
That’s where a new or improved impact bed comes in handy. Our impact beds are designed to better absorb the stress that materials and product put on conveyors. This is especially important for conveyors that move bulk and jagged product in mines or quarries.
Good impact beds also help eliminate product spills and dust accumulation–especially in the load zone–keeping operations running longer and minimizing downtime.
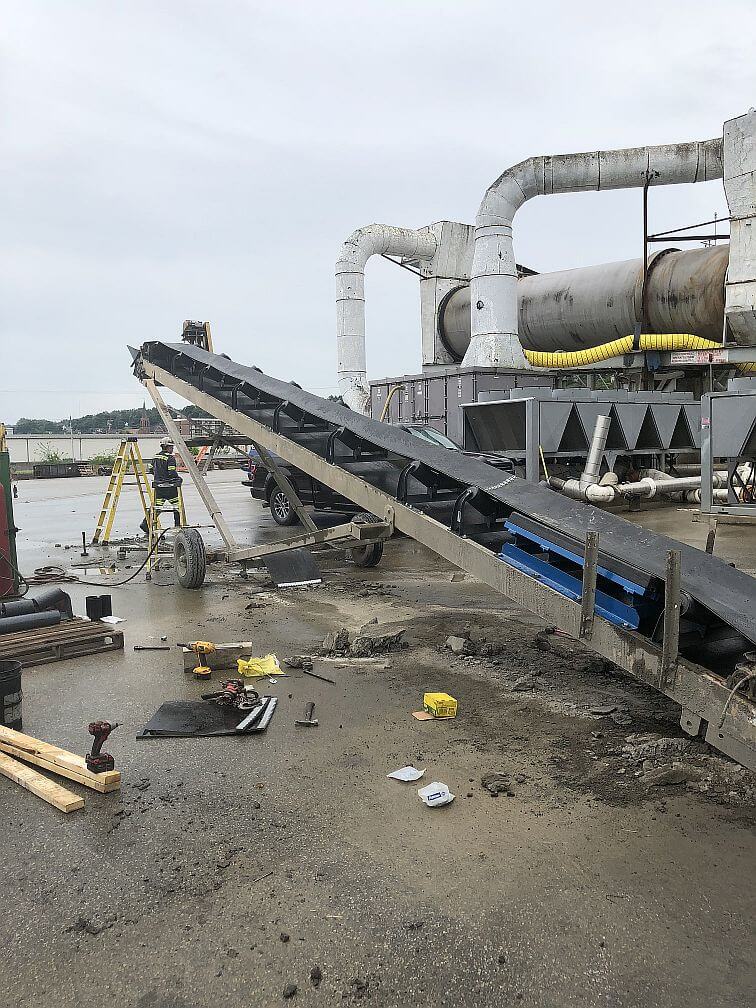
Our impact beds are best installed at conveyor transfer and feed points to reduce the risk of puncture damage to conveyor belts. We have impact beds to fit any specific application and any type of conveyor. If you need assistance choosing which impact bed is best for your particular conveyor, contact our team today for help.
More about West River Conveyor impact beds
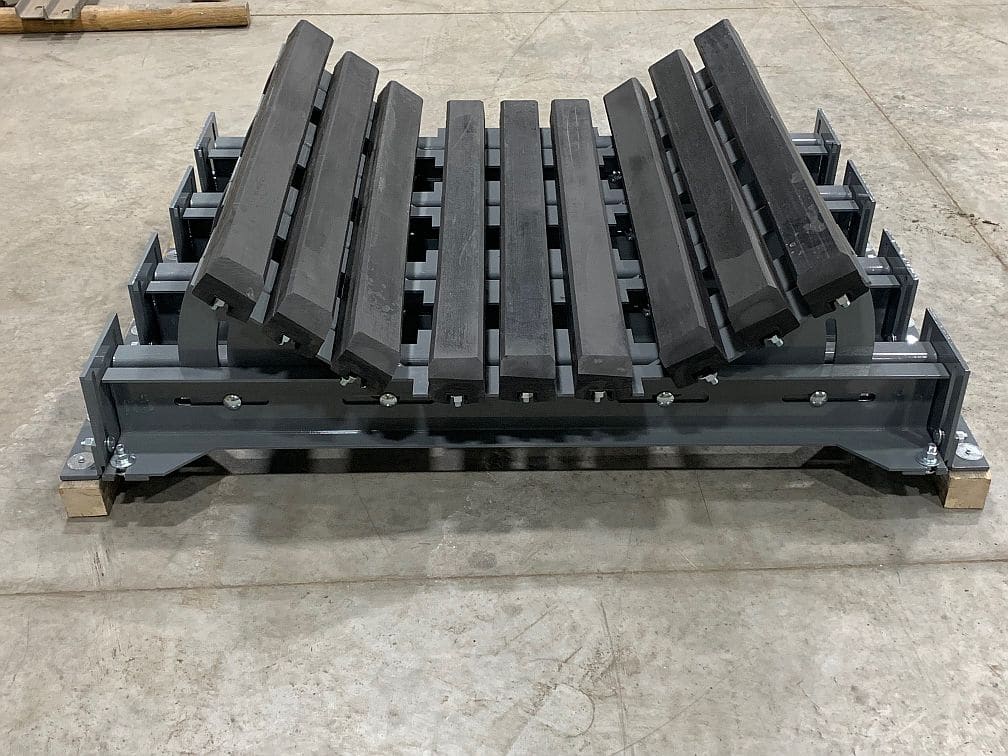
Our impact beds are made from heavy-duty structural steel, and each is designed to CEMA standards. They’re fixed or adjustable and designed to last.
Here’s a look at more information about our line of industry-leading impact beds and the advantages your operations can reap from incorporating them into your conveyor:
Advantages of impact beds
Impact beds are ideal for installation at conveyor feed and transfer points, as they work to prevent belt damage and belt sagging at heavy product loading points. But there are many other advantages of installing impact beds to complement your conveyors’ operations. These include:
Robust & impact resistant: Impact beds made from heavy duty structural steel and are robust and impact resistant; two attributes that help them stand up to the demanding materials and load quantities that many work with on a regular basis.
Extended life of skirting: Our impact beds’ robust properties don’t just prevent conveyor belt damage, but they also help extend the life of skirting.
Reduced spillage: In addition to skirt sealing, West River Conveyors’ impact beds also help reduce product spillage.
Reduced maintenance costs: Reduced product spillage, dust accumulation, and belt damage directly correlate to less overall maintenance. This means you won’t just save money on maintenance and repair costs, but you’ll also save by reducing conveyor downtime. It all adds up to improve the bottom line and reduce operating expenses.
Overall safer work environments: Impact beds help promote a safer, healthier overall work environment. Studies show that a safe, healthy work environment can directly translate into more productive workers.
The benefits of impact beds lead to a more productive, leaner work environment. Impact beds help minimize maintenance, extend product life and help keep product moving consistently from Point A to Point B along the conveyor belt.
Improve belt longevity and reduce maintenance costs with the Impact Bed Tail Section, which uses low-friction UHMW polyethylene bars to absorb impact energy and protect your conveyor belt in high-stress loading zones.
Get better impact beds to protect and improve your conveyor structure
Tired of your conveyor belt sagging, or always requiring replacement or repair? Is dust accumulation a problem around heavy product loading points? Don’t just replace your impact bed with any model, replace it with the right one.
At West River Conveyors, every one of the impact beds we offer is designed to work efficiently and effectively for long, extended periods of time.For availability and pricing on impact beds, please call 800.332.2781 or Contact Us today.
What Our Customers are Saying
“I would like to express my appreciation and gratitude for the exceptional support provided by Russ during a recent troubleshooting effort. His availability, technical expertise, and proactive approach were instrumental in resolving the issues efficiently and effectively. Russ’s dedication to fostering and maintaining strong, long lasting professional relationships surpasses the typical sales mentality I have grown used to dealing with elsewhere. His commitment to his customers and consistent follow through has built a foundation of trust that I professionally continue to rely on. Having someone so dependable and relationship focused adds tremendous value, and it speaks volumes about the culture and professionalism of West River as a whole. Please extend my appreciation to Russ for his outstanding work and continued partnership.”
– Regina Tuberville, Sr. Mine Engineer
“I have had excellent success with everything I have purchased from West River. The service is great! I have called after hours and received the same top-notch service. The pulleys that I bought have been top-quality and are doing very well. I recently had some alignment work done on our slope belt, with the same high quality workmanship. I would recommend West River to anyone needing gearboxes, pulleys, alignment, or other conveyor components.”
– Steve Bjork, Preparation Plant Maintenance Chief
“West River is a friend to the mining industry, supplying quality components at a competitive price!”
– Barry Tackett, Operations Manager, Mountain Aggregates
“From the beginning, we wanted to standardize our conveyor equipment. We knew we wanted to minimize the number of spare parts and pulleys. This has been the only time in my career I’ve been able to accomplish this task. The good relationship that we’ve developed with West River is attributed to the genuinely good people that run the company. In my experience, many vendors are primarily interested in maximizing their profit margin but I truly believe the team at West River has the best interest of the customer at heart.”
– Brad Rigsby, General Manager, Black Panther Mining
“West River’s conveyor systems have given us a great level of reliability. In the years that we have been using them as our supplier, we have not had a single breakdown, no quality issues, and no under-design problems. West River’s dedication to excellence in customer service is exceptional. All phone calls and emails are replied to in a timely manner and deadlines are always met even when they may seem unachievable.”
– Coley Burgess, Mine Engineer, Mosaic Company
Custom Overland and Underground Mining Conveyor Equipment
For most mining operations, the relationship with a conveyor supplier ends at commissioning. The system is installed, it runs, and the paperwork gets filed away. At West River Conveyors, that's read more »
Leaching is often discussed in terms of chemistry—solutions, reactions, and recovery rates. But behind every successful operation is a material handling system that keeps everything moving at the right pace. read more »
When a conveyor system isn’t performing as expected, the first instinct is often to look at belt speed, capacity, or wear components. But in many cases, the issue starts upstream—inside read more »
This website uses cookies to improve your experience. We'll assume you're ok with this, but you can opt-out if you wish. Cookie settingsACCEPT
Privacy & Cookies Policy
Privacy Overview
This website uses cookies to improve your experience while you navigate through the website. Out of these cookies, the cookies that are categorized as necessary are stored on your browser as they are as essential for the working of basic functionalities of the website. We also use third-party cookies that help us analyze and understand how you use this website. These cookies will be stored in your browser only with your consent. You also have the option to opt-out of these cookies. But opting out of some of these cookies may have an effect on your browsing experience.
Necessary cookies are absolutely essential for the website to function properly. This category only includes cookies that ensures basic functionalities and security features of the website. These cookies do not store any personal information.