Fly ash is a difficult material to move, especially by truck. When it’s dry it blows away easily, creating a mess and environmental problems that lead to complaints and mechanical breakdowns. A better solution for coal and fly ash remediation is a conveyor system designed with purpose.

The EPA has mandated that all U.S. power plants have a solution in place for the safe removal and permanent storage of their fly ash and bottom ash, but the process can be complex and risky.

West River Conveyors builds conveyors for coal and fly ash remediation, systems specifically tailored to the materials being conveyed. The custom systems we create for the coal and fly ash remediation industry use high-quality parts that maximize reliability and up-time.

Share the details of your fly ash handling needs with us and we’ll follow up quickly to help you implement a solution.

Contact One of Our Conveyor Specialists

Recommended Products
mining industry that large or huge machine used

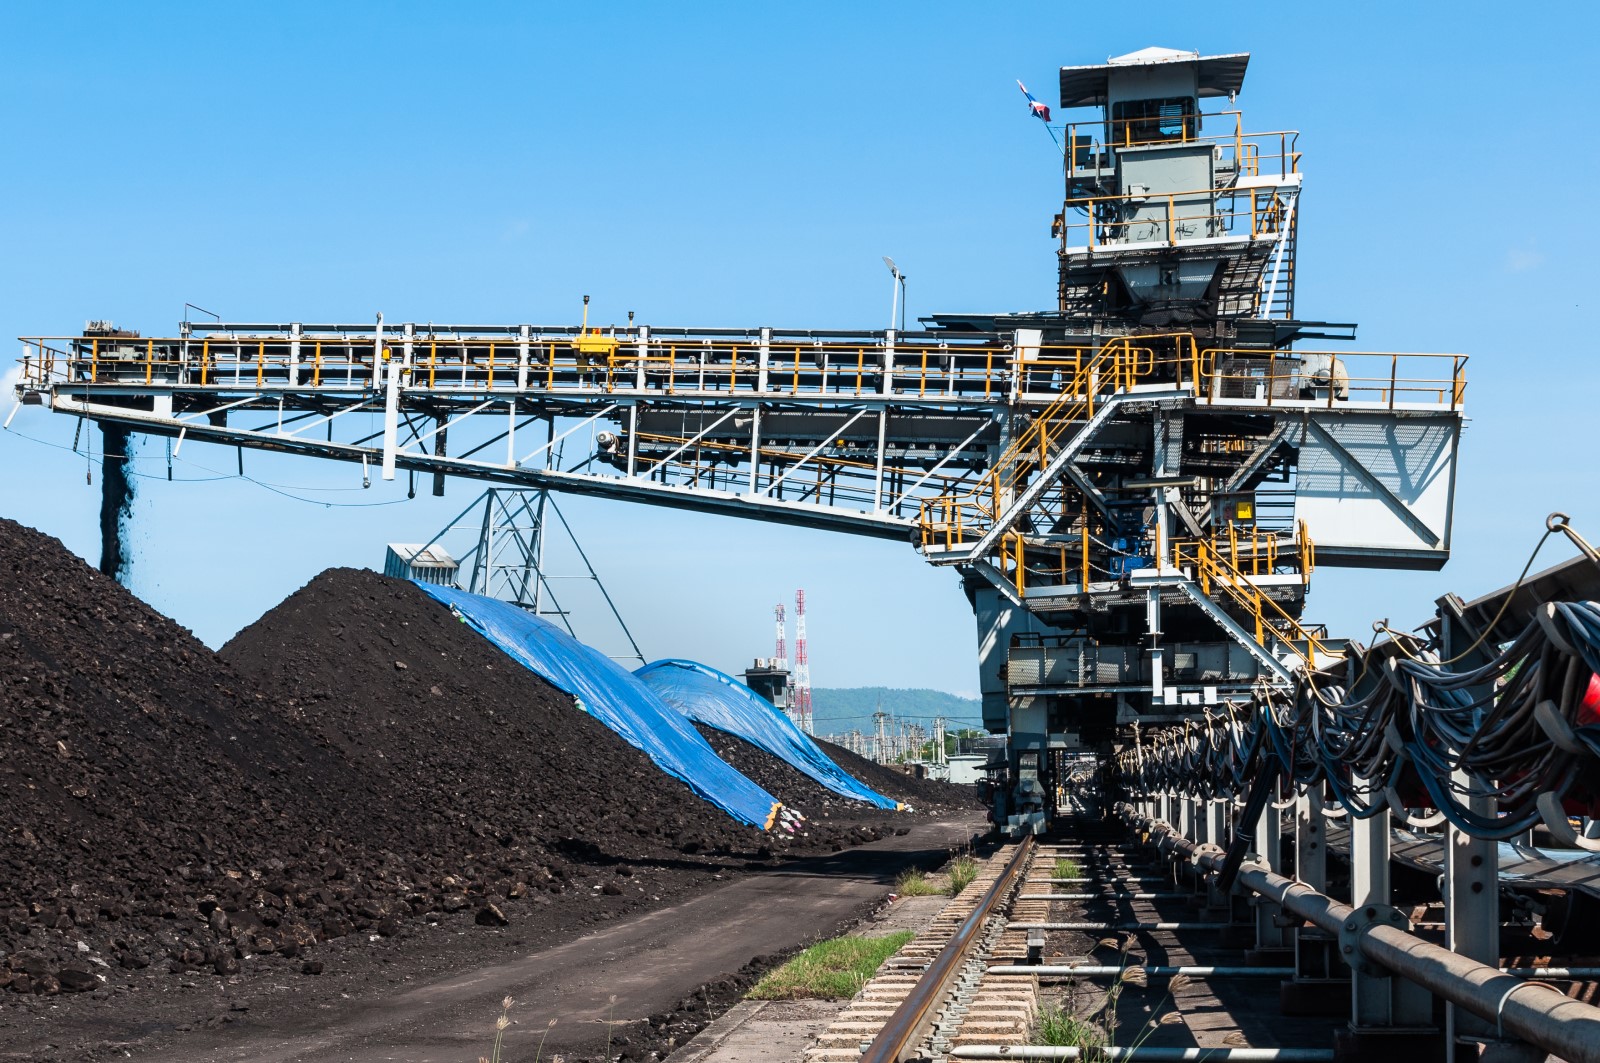
Stacker Conveyor

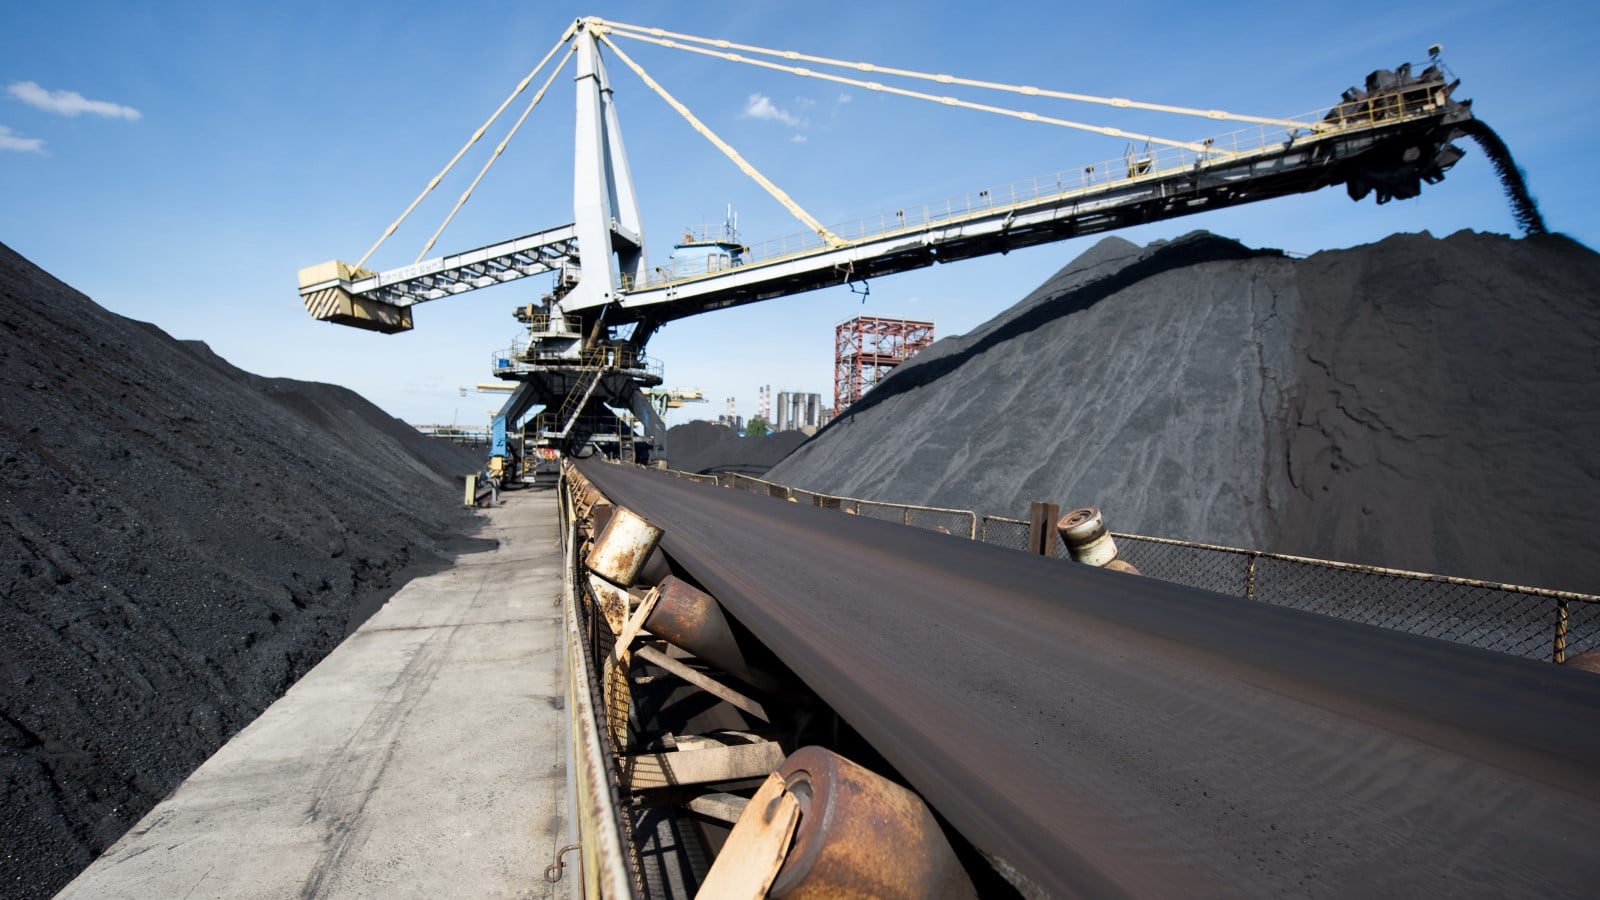
West River Conveyors understands the challenges of stockpiling. Whether you’re looking for a conventional, radial, telescoping, or telescoping-radial stacker conveyor, we have the expertise to design and build a custom solution that meets your needs.

LEARN MORE
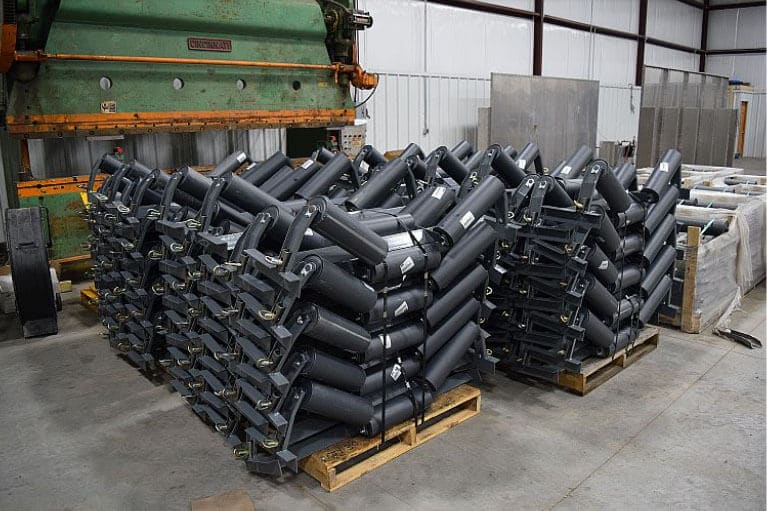
Conveyor Structure

Our full range of highly engineered underground conveyor structure will provide you with a turnkey conveyor solution. Our underground rigid, catenary or wire structure comes in CEMA B, C, D, E, and E+ arrangements and can be used for longwall and room & pillar operations.

LEARN MORE
Surface Conveyor Belts

Aggregate materials can cause rips and tears in inferior belts. We have a wide range of heavy-duty surface conveyor belts to help decrease unplanned downtime while safely getting your aggregate from Point A to Point B.

LEARN MORE

About Our Fly Ash Conveyors

Conveyors for coal and fly ash remediation are often extended, modified, or even repurposed. When you’re investing in new equipment, it must integrate seamlessly with what you already have. Spare parts availability and inventory are also significant concerns for fly ash conveyor system operators.

West River Conveyors understands the importance of these issues—we work with operators to minimize the complexity and variety of equipment used. When specifying a new system or additional equipment for you, we look at what’s in place now, and together we create a strategy to minimize your spare parts inventory.

Custom Fly Ash Handling Conveyor Packages

Fly ash remediation can be a complex undertaking. A custom conveyor system will handle more per hour than a trucking fleet while generating less dust and noise.

We can help add to or upgrade an existing system or deliver a completely new system engineered to meet your needs and expectations.

Custom packages commonly include the following components:

Fly Ash Conveyor Accessories

When dry, fly ash is a light dust that readily coats surfaces with its combination of silicon dioxide, aluminum, and calcium oxide. When wet it becomes a heavy slurry that’s especially difficult to transport.

We can recommend accessories and upgrades that will improve safety and reliability while reducing operating costs and downtime. Some conveyors for coal and fly ash remediation need unique accessories—the most common include:

For availability and pricing on conveyor accessories, call 800.332.2781.

Companies We’ve Helped

What Our Customers are Saying

“I would like to express my appreciation and gratitude for the exceptional support provided by Russ during a recent troubleshooting effort. His availability, technical expertise, and proactive approach were instrumental in resolving the issues efficiently and effectively. Russ’s dedication to fostering and maintaining strong, long lasting professional relationships surpasses the typical sales mentality I have grown used to dealing with elsewhere. His commitment to his customers and consistent follow through has built a foundation of trust that I professionally continue to rely on. Having someone so dependable and relationship focused adds tremendous value, and it speaks volumes about the culture and professionalism of West River as a whole. Please extend my appreciation to Russ for his outstanding work and continued partnership.”

– Regina Tuberville, Sr. Mine Engineer

“I have had excellent success with everything I have purchased from West River. The service is great! I have called after hours and received the same top-notch service. The pulleys that I bought have been top-quality and are doing very well. I recently had some alignment work done on our slope belt, with the same high quality workmanship. I would recommend West River to anyone needing gearboxes, pulleys, alignment, or other conveyor components.”

– Steve Bjork, Preparation Plant Maintenance Chief

“West River is a friend to the mining industry, supplying quality components at a competitive price!”

– Barry Tackett, Operations Manager, Mountain Aggregates

“From the beginning, we wanted to standardize our conveyor equipment. We knew we wanted to minimize the number of spare parts and pulleys. This has been the only time in my career I’ve been able to accomplish this task. The good relationship that we’ve developed with West River is attributed to the genuinely good people that run the company. In my experience, many vendors are primarily interested in maximizing their profit margin but I truly believe the team at West River has the best interest of the customer at heart.”

– Brad Rigsby, General Manager, Black Panther Mining

“West River’s conveyor systems have given us a great level of reliability. In the years that we have been using them as our supplier, we have not had a single breakdown, no quality issues, and no under-design problems. West River’s dedication to excellence in customer service is exceptional. All phone calls and emails are replied to in a timely manner and deadlines are always met even when they may seem unachievable.”

– Coley Burgess, Mine Engineer, Mosaic Company

previous arrow
next arrow
Slider

RECENT PROJECTS

Conveying Sand For A Cottageville, SC Aggregate Producer

Discover how West River Conveyors designed and custom-built a 1,000-foot overland conveyor system for this large-scale aggregate operation.

read more

The Top 3 Conveyor Issues & How To Avoid Them

Explore the three most common conveyor issues and how to take proactive steps to prevent them from happening.

read more

How Much Does An Overland (Surface) Conveyor System Cost?

Read more about what’s included in an overland conveyor package and how application characteristics influence cost.

read more

Success Stories

Conveyors and Machinery to Match Your Application

We have 40 years of experience designing, building, and installing customized conveyor systems at West River Conveyors. In addition to conveyors for coal and fly ash remediation, the systems we have designed, installed, and upgraded are at work in underground and above ground mining industries from coal to salt, sand, aggregate, potash, and trona. Our reliable products and dedication to customer service make us the go-to choice for solving your toughest challenges. Contact us today to speak with a specialist who will take the time to listen to your concerns and provide you with an intelligent and competitively priced solution.


We Offer Free Estimates!